Manufacturing technology leadership
Fractional CTO for Manufacturing: Systems and Hiring
Scope manufacturing CTO leadership around ERP, production information, supplier choices and pilots. Includes a worked order-status example and hiring questions.
- By
- Fractional CTO Experts
- Published
- 2026-09-09
- Reviewed
- 2026-09-09
- Reading time
- 14 minutes
A fractional CTO can help a manufacturing business make consequential technology decisions when it needs senior leadership for a defined portion of time. The mandate may involve business systems, production information, supplier choices or a modernisation plan. The arrangement works best when the required authority, specialist participation and operating responsibilities are explicit, and the business has people available to implement the resulting decisions.
This guide explains how to evaluate that fit without treating manufacturing as a generic software project. Fractional CTO Experts is an executive network and matching platform. You can request candidates with the relevant systems, site and working requirements, then verify each person's experience and availability. This page does not promise a manufacturing delivery team, plant-engineering capability or a particular operational result.
Begin with the business decision and its production context
Name the decision the company cannot currently make well. It may be choosing how to connect production information with order management, evaluating a replacement business application or deciding which data problem to address before pursuing automation. Explain the consequence of getting the decision wrong and the people who understand that consequence. This creates a more useful search brief than asking for broad digital transformation experience.
Describe the manufacturing environment at the level needed to judge fit. A company assembling configurable products has different information needs from one producing continuous batches. A single-site operation differs from a group with several plants and local systems. The candidate should be able to explain which parts of their experience transfer and which assumptions require further investigation.
Separate the product-engineering and business-systems responsibilities. Expertise in designing an excellent physical product does not automatically establish experience selecting or integrating business software. Equally, an executive with strong software experience may need substantial support from plant, controls, maintenance, quality and safety specialists. Define the actual leadership gap and the team required around it.
Ask who can authorise changes that affect production commitments. A fractional CTO may coordinate evidence and recommend a direction without having authority to approve a plant change. Make that boundary clear before the engagement begins. Technology leadership should help the relevant decision-makers understand the options, not replace responsibilities that belong to qualified people in the operating organisation.
Map business systems and production information separately
Siemens' explanation of ERP and MES distinguishes business planning and resource information from the execution of manufacturing operations. It also describes information flowing between them. That is useful context for an integration discussion, but it does not mean every manufacturer needs the same products or system boundaries. Start with your actual processes and information owners.
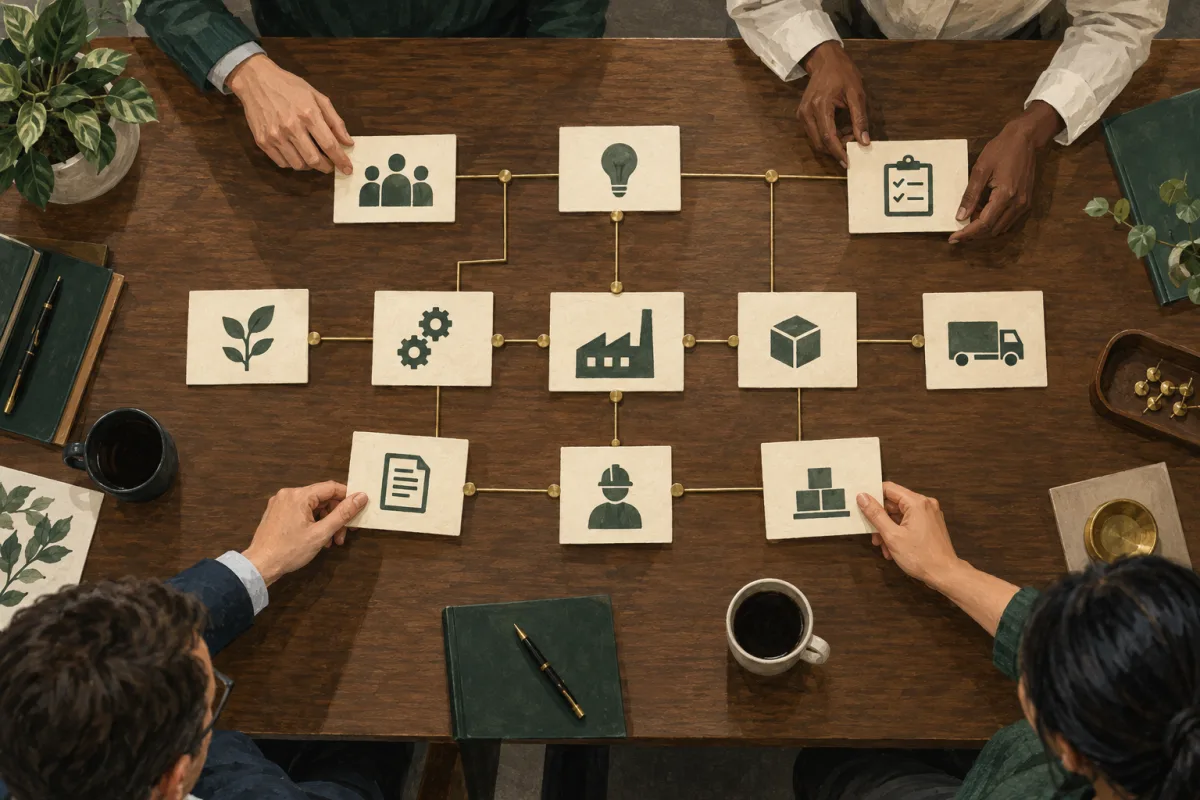
List the important information exchanges. An order, product definition, production record or material movement can pass through several systems and teams. Identify where the authoritative information originates, where it changes and who relies on it next. Include spreadsheets and manual records when they form part of the real process. A diagram that omits them may hide the very dependency the project needs to resolve.
| Information area | Question to resolve before integration | Business owner to involve |
|---|---|---|
| Product and order definition | Which version and requirements govern this work? | Product, planning and relevant customer-facing teams |
| Production status | What event changes the reported state? | Production and planning |
| Quality disposition | Which condition permits the next agreed use? | Quality and the relevant operating authority |
| Inventory availability | Which quantities are usable for which purpose? | Inventory, planning and fulfilment |
| Cost and reconciliation | How are differences investigated and explained? | Finance and operations |
| System ownership | Who maintains the interface and resolves exceptions? | Technology and the receiving service owner |
Treat this table as a starting point for a conversation, not a complete manufacturing data standard. Define the terms the company actually uses and the responsibilities that make them reliable. The same label can mean different things to a planning system, an operator and a customer-service team. Resolve that ambiguity before treating an automated transfer as trustworthy.
Worked example: completed does not always mean available to ship
Imagine a hypothetical manufacturer investigating conflicting order-status reports. In a deliberately simplified snapshot, 200 units have been processed: 160 are accepted for the intended shipment, 20 are held for a quality decision and 20 are scrapped. These categories are mutually exclusive in this example. There are no other allocations or movements included, and the figures are not a client result or operating recommendation.
One production report describes the 180 non-scrapped units as completed. An integration sends that number to a business application, where it is interpreted as available to ship. The arithmetic in the production report may be internally consistent, but the meaning changes at the interface. The destination has counted the 20 held units as if they had the same disposition as the 160 accepted units.
A useful technology leader investigates the definitions and responsibilities before proposing a new dashboard. Who decides the quality status? When is that decision recorded? Which event makes the information available to planning or fulfilment? What happens when the status changes? The people who own the operating process must establish those answers; a technical mapping alone cannot decide them.
The team might agree separate fields or events for produced quantity, quality disposition and usable inventory, depending on the actual system design. It should then test representative records and exceptions in an appropriate environment. The important evidence is whether the receiving users interpret the result correctly and whether the relevant controls and responsibilities remain intact.
In this simplified snapshot, only the 160 accepted units meet the example's stated shipment condition. The 20 held units require the relevant decision, while the 20 scrapped units belong in their separate category. A proposed solution should preserve those distinctions and explain how later updates are reconciled. Moving an ambiguous number faster would make the discrepancy more immediate, not make the business information more reliable.
Respect the differences between IT and operational technology
NIST SP 800-82 Revision 3 addresses operational technology security in the context of performance, reliability and safety requirements. Its scope includes systems that interact with the physical environment. Use this as a reason to involve appropriate specialists and review the actual operating context. This buyer guide is not a plant security assessment or an instruction to modify control systems.
Identify where the proposed work touches production equipment, control systems or the information those systems depend on. Ask the qualified owners to explain the boundary and the review required. An executive should recognise when a normal business-application assumption does not transfer to the operating environment. The engagement must provide a route for resolving these questions before implementation commitments are made.
Confirm how suppliers and internal teams participate. The company may depend on equipment vendors, systems integrators and people with specialised knowledge of the installed environment. Record their responsibilities and the evidence required from them. A broad technology brief should not silently assume that one part-time executive can supply every discipline needed for consequential plant work.
Keep the scope of assessment and change explicit. A planning conversation can use existing records and interviews; deeper inspection or implementation requires the appropriate access and authorisation. Agree those boundaries with the relevant owners. The objective is a clear decision process that supports the operating organisation, rather than a generic checklist presented as proof that a physical environment is safe.
Compare integration, configuration and replacement options
Ask what the company needs to change before deciding which software to buy. The problem may arise from unclear definitions, an unsupported interface, an unsuitable workflow or a platform limitation. These can lead to different recommendations. A supplier demonstration should be evaluated against the actual problem and the information the business needs to maintain.
Compare feasible options using the same responsibilities and constraints. Improving an existing process may reduce transition work but retain an important limitation. A replacement may address that limitation while requiring migration, training and new operating support. Custom development may offer flexibility while creating a capability the company must continue to maintain. Explain the dependencies behind each option.
Include the receiving users in the evaluation. A technically plausible solution can still fail to support the tasks people perform during ordinary work and exceptions. Use representative cases, including the difficult ones the current process handles poorly. Ask users to explain the result in their own terms rather than confirming only that a screen or interface exists.
Record why the selected option is preferable under the current assumptions. Identify the evidence that would change that choice. This makes the decision easier to review when scope, costs or operating conditions change. It also helps a future leader understand why the company configured, integrated or replaced a system instead of assuming the earlier team overlooked the alternatives.
Use a bounded pilot to test the important assumptions
Choose a pilot scope that can answer a consequential question. A smaller scope is useful when it limits complexity while preserving the dependency you need to understand. For the order-status example, the pilot might focus on a representative information path and agreed records. The operating owners should determine an appropriate environment and process for the work.
Specify the expected evidence before the pilot begins. Include how source records are interpreted, how exceptions are handled and who can explain the destination information. State what is excluded. A pilot should not be called successful merely because data moved between applications if the central question concerns whether users can rely on its meaning.
| Pilot question | Evidence to agree | Decision supported |
|---|---|---|
| Do the definitions remain consistent? | Representative records traced across the agreed path | Whether the mapping is usable |
| Can exceptions be recognised? | Relevant non-routine cases and their handling | Whether additional work is required |
| Can users explain the output? | Receiving-team review using actual task context | Whether training or design needs to change |
| Is responsibility clear? | Named owners for source, interface and destination issues | Whether the process can be operated |
| What remains untested? | Explicit scope and limitation record | Whether to expand, revise or stop |
Review the pilot with the people who will use and maintain the result. Ask what was learned and which assumptions proved wrong. The next step may be a revised design, another bounded test or a decision not to proceed. A useful fractional CTO makes that choice clearer rather than treating the pilot as a ceremony that must justify a preselected rollout.
Plan changes around the receiving operation
A systems plan should identify the people, information and operating arrangements needed at transition. Discuss the sequence with the relevant production and business owners. The appropriate timing and approval process depend on the environment. A software completion date is not automatically a suitable date for the business to adopt the resulting process.
Ask how the team will recognise an unacceptable result and who can decide the next action. Review the dependencies involved in continuing, pausing or changing the plan. The qualified owners should establish any operating procedures and limitations. Avoid accepting a generic recovery promise that has not been examined against the actual systems, information and commitments involved.
Include preparation and follow-through in the resource plan. Users may need to review records, practise representative tasks or help resolve discrepancies. Suppliers may need to provide specific evidence or support. If these activities are omitted from the proposal, the company may discover that the visible implementation work was only part of what was needed to make the change usable.
Evaluate the business case without assuming a guaranteed return
State what improvement the company expects and how it would be observed. Reducing repeated data entry, clarifying order status and improving a planning decision are different outcomes. Establish the starting condition and the people who can verify it. Do not turn an attractive vendor benefit into a forecast without examining whether the relevant mechanism exists in your operation.
Separate costs and dependencies that occur once from those that continue. Consider implementation, company participation, data preparation, training, support and the ongoing ownership of the selected approach. Work with finance and the operating team to compare proposals on a consistent basis. A lower software price may be offset by work that still needs to be done internally.
Treat uncertainty as part of the decision. The company may not yet know how much time a particular discrepancy consumes or how often an exception occurs. Gather suitable evidence or state the limitation. A model with explicit assumptions can support a bounded next step; an unsupported promise of a standard return or failure-rate reduction should not determine the investment.
Interview for manufacturing judgment and collaboration
Ask candidates to describe a relevant decision they personally helped an organisation make. Explore the type of operation, the systems involved, the people who owned the process and the limits of the candidate's responsibility. Experience in one manufacturing setting can be valuable without proving suitability for every production environment or specialist discipline.
Use the order-status example to examine how a candidate approaches ambiguity. Notice whether they investigate business definitions, quality responsibility and the information path before proposing an integration product. Ask what additional expertise they would involve and what evidence would make them change their initial recommendation. The questions can reveal more than a long list of platform names.
Discuss a disagreement with a plant, quality, finance or supplier team. Ask how the candidate clarified the decision and handled evidence that contradicted their first view. Technology leadership in this setting depends on working effectively with people who understand different parts of the operation. The executive should be able to recognise those contributions and explain the boundaries of their own expertise.
Verify personal contribution and relevant references where available. A claimed transformation result or a recognisable manufacturer on a résumé does not establish what the person actually owned. Keep unverified outcomes separate from evidence you can inspect. The search should make the candidate's fit clearer without manufacturing a certainty that neither party can support.
Choose an engagement model the company can support
Define which decisions recur and which require concentrated work. A fractional arrangement may suit a sequence of leadership reviews with implementation continuing between sessions. A major transition may require more continuous coordination or another engagement model. State the availability required by the actual work instead of assuming that every manufacturing technology mandate fits a monthly retainer.
Name the internal and external people expected to act on decisions. An executive introduction is not a substitute for systems implementation, plant expertise, data ownership or user participation. Confirm how those resources will be supplied and who can resolve a conflict between priorities. A leadership agreement is more credible when its dependencies are visible from the beginning.
Compare the executive's proposed terms separately from platform pricing. Request a current scope with reserved capacity, site attendance where required, additional work and supporting resources explained. This guide does not provide a verified manufacturing executive rate card, a guaranteed roster or a fixed implementation timetable. Confirm the actual arrangement with the relevant parties.
Review the first phase and preserve continuity
At the first review, ask whether the relevant decisions are clearer, the information owners agree on important definitions and the team understands the next commitments. Examine the evidence behind any claimed improvement and the limits of the work completed. Use the review to select the next phase, change the scope or end an arrangement that does not fit.
Maintain company access to the important system maps, definitions, decisions and responsibility records under the agreed terms. Another qualified person should be able to locate the basis for the next decision and identify who owns an unresolved issue. A handover assembled only at the end can miss the reasoning that made the plan usable.
Have the receiving team demonstrate a representative review or update. In the order-status example, that could mean explaining a record through the agreed information path and identifying the appropriate owner of an exception. Resolve missing context before the transition ends. The engagement should leave the company better able to continue the work with its own operating responsibilities intact.
Frequently asked questions
What does a fractional CTO do for a manufacturer?
The mandate can help management make consequential decisions about business systems, production information, suppliers and modernisation. Define the actual scope, authority, specialist participation and implementation resources. A fractional executive does not automatically supply plant engineering, controls, safety expertise or a complete delivery team.
Can a fractional CTO help with ERP and MES integration?
A suitably experienced leader can help clarify the business question, information ownership, system responsibilities and supplier decisions. The company still needs qualified implementation and operating participants. Test representative records and exceptions, including what data means to the receiving users, rather than accepting data movement alone as proof of a useful integration.
Why do production and inventory figures sometimes disagree?
Investigate the definitions, timing and responsibilities behind the figures. In this guide’s invented example, completed non-scrapped units include items still held for a quality decision, while available-to-ship has a narrower meaning. The example illustrates a possible mapping problem; the actual cause must be established from the manufacturer’s records and process.
Does a manufacturing CTO replace operational technology specialists?
No. Identify where the mandate touches equipment, control systems or relevant operating dependencies, and involve appropriately qualified owners and specialists. Clarify assessment and change authority. This guide does not provide a plant security or safety assessment, and a general technology title does not establish every required competence.
How should a manufacturer evaluate a technology pilot?
Agree the question, representative scope, evidence, operating owners and limitations before starting. Review whether definitions remain consistent, exceptions can be handled and receiving users understand the result. Use the findings to decide whether to revise, expand or stop, without treating one bounded pilot as proof that every site or process is covered.
How much does a fractional manufacturing CTO cost?
Request current proposals for the actual decisions, reserved capacity, site attendance, implementation support and additional work. Compare platform fees separately from executive terms. This guide does not publish a verified manufacturing rate card or guarantee a roster, implementation timetable or operational return.
Sources and further reading
Turn research into a mandate
See the cost and hiring model before you shortlist.
Use the free calculator, then save a candidate search or post a transparent role when the mandate is ready.